How precision manufacturing improves accuracy in solar module testing
auth.Dr. Liang CheTime
Oct 03, 2026Click Count
A solar module can pass through electrical testing with an apparently stable result and still carry uncertainty introduced by the test setup itself. This often becomes visible when repeated measurements differ more than expected, when a module must be repositioned after an interruption, or when results from two stations cannot be reconciled without re-testing. In a production or procurement review, the immediate question is not only whether the module met its target value, but whether the measurement system had enough mechanical and electrical control to make that value defensible.
Precision manufacturing improves accuracy in solar module testing by reducing variation in the hardware that holds, contacts, positions, heats, cools, and measures the module. Tight dimensional control in fixtures, probe assemblies, motion systems, reference surfaces, and calibration interfaces makes repeatability easier to demonstrate. It does not replace valid test methods, calibration, irradiance control, or competent operators. Instead, it removes avoidable physical sources of error that can otherwise distort electrical output, mechanical-load, insulation, and durability assessments.
Where mechanical variation enters a module test
PV test procedures are often discussed in electrical terms: current-voltage tracing, irradiance level, spectral response, temperature correction, or insulation resistance. Yet each of those measurements depends on a physical setup. A module that sits slightly differently in a flash tester, receives unequal contact pressure at its terminals, or bows on an uneven support can produce data that reflect the station as much as the product.
This is particularly relevant for large-format modules. Their greater surface area, longer frames, and higher current paths make them more sensitive to support geometry, handling alignment, cable routing, and terminal contact conditions. The issue is not that every small deviation automatically invalidates a result. The concern is whether the deviation is controlled, repeatable, and known well enough to be separated from actual module behavior.
Precision-engineered equipment addresses this through defined datums, stable reference surfaces, controlled clamping forces, repeatable actuator travel, and contact components manufactured within appropriate tolerances. When a module enters the station, its position should be established by intentional reference points rather than by operator judgment or incidental contact with loosely fitted stops.
Typical sources of test-induced variation
- Fixture geometry: Nonparallel rails, worn locating stops, or unsupported spans can introduce module twist or uneven bearing loads.
- Electrical contacts: Probe wear, inconsistent spring force, oxidized surfaces, or cable strain can change contact resistance during IV testing.
- Motion accuracy: Misaligned gantries and poorly controlled travel can alter the distance, angle, or dwell time between a sensor, light source, and module surface.
- Thermal interfaces: Uneven contact with a temperature sensor or uncontrolled cooling around the module can weaken temperature-dependent corrections.
- Repeat positioning: A module moved between measurements may not return to the same plane or reference location without positive locating features.
These effects can be subtle. A station may appear functional in normal use while still generating an avoidable spread in repeated results. For technical evaluation, a credible test system should make its mechanical repeatability visible through inspection records, calibration routines, component replacement criteria, and comparison of measurements over time.
Accurate IV measurement begins before the flash
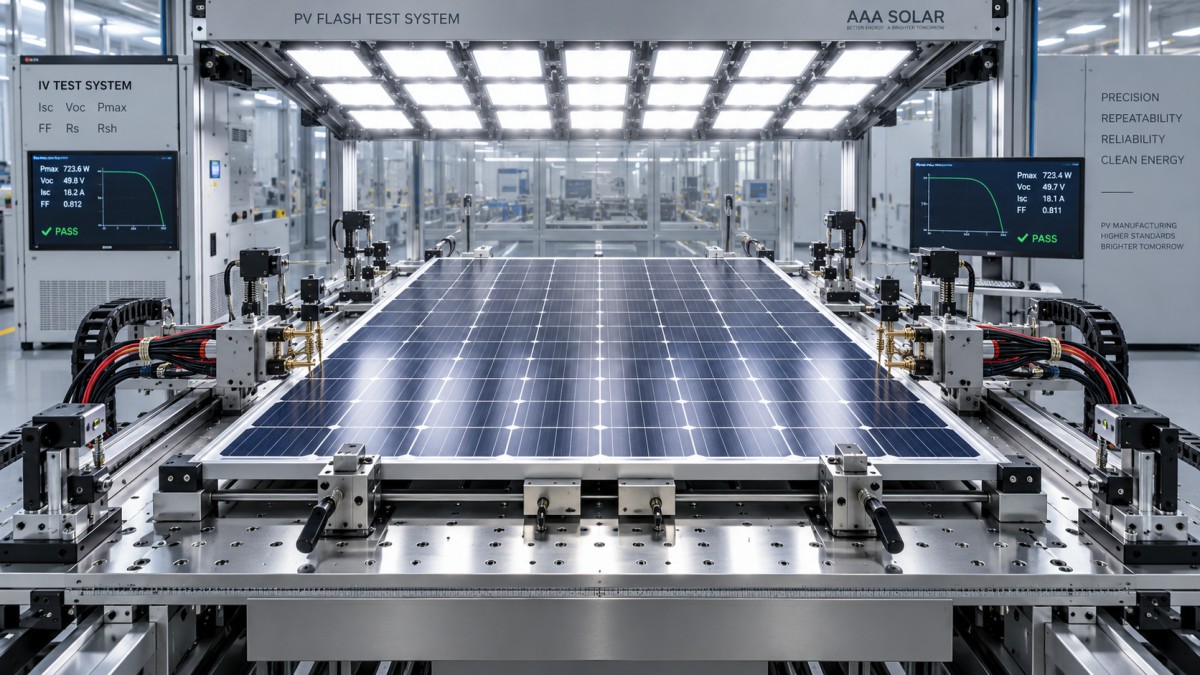
Flash testing is a useful example because it combines optical, electrical, thermal, and mechanical variables in a short measurement event. The tester must deliver a defined irradiance condition, while the module must be connected consistently enough for the measured current and voltage to represent its actual electrical behavior. Precision manufacturing improves the physical conditions around that event.
The module support plane should prevent unintended bending while avoiding unnecessary constraint. A frame supported at only a few inconsistent points may deflect differently from one loading cycle to another. Conversely, excessive clamping can impose stress that is not representative of normal module condition. A properly designed fixture uses known support locations and controlled restraint so the module remains stable without introducing uncontrolled mechanical load.
Terminal connection is equally important. At high module currents, small changes in resistance at connectors, clips, busbars, or test leads can affect the observed voltage and fill factor. Contact systems should apply repeatable force and maintain alignment with the intended connection geometry. Their materials and surface condition also matter: a contact that is mechanically accurate when new may become less reliable as it wears, contaminates, or loses spring performance.
Precision manufacturing does not mean assuming that a fixed probe position will work for every module design. Module dimensions, junction-box locations, lead lengths, connector formats, and frame profiles vary. The better approach is a fixture architecture with controlled adjustment ranges, documented datum references, and verification after any changeover. Adjustment without measurement simply transfers uncertainty from one part of the station to another.
What evaluators should examine around electrical contact
Mechanical-load and durability tests depend on fixture fidelity
Mechanical-load testing, cyclic loading, and related durability evaluations require even more scrutiny of the fixture. The test apparatus is not merely a holder; it is part of the load path. If the support arrangement differs from the intended boundary condition, the module may experience stress concentrations, local bending, or asymmetric deflection that are not attributable to its design.
For example, a support frame with insufficient flatness can create a high point under a module. During loading, that point may concentrate stress in the glass, laminate, frame, or mounting region. A result from such a setup may be difficult to interpret: apparent damage could be a genuine product weakness, but it could also arise from a nonrepresentative fixture condition. Precision-machined support structures and verified loading surfaces reduce this ambiguity.
The same principle applies to pneumatic or mechanical actuators. Their placement, stroke control, and load-transfer interfaces should be repeatable across the test area. When multiple loading points are used, geometric consistency helps prevent one zone from receiving a disproportionate share of the applied force. Load cells and control software remain essential, but accurate force readings alone do not prove that the force reached the module uniformly. The mechanical stack-up must be considered as a complete system.
During a technical review, it is useful to distinguish between measured load and delivered load condition. The first concerns the instrument reading. The second concerns how that load is distributed through pads, supports, frames, and contact surfaces. Precision manufacturing supports both by limiting dimensional scatter among these components and by making their geometry verifiable.
Why tolerance control matters for IEC-oriented validation
IEC test requirements define methods and acceptance conditions for many aspects of PV module qualification and performance evaluation. They do not eliminate the need for careful equipment design. A procedure can be followed in form while the physical setup still introduces variation that weakens comparability between runs, samples, or laboratories.
For this reason, tolerance should be considered in context rather than treated as a single number. The critical question is which dimensions influence the test result. A tight tolerance on a cosmetic cover may have little relevance. A smaller deviation in a module locating edge, actuator height, support rail position, or sensor mounting plane may be much more consequential because it changes the module’s orientation, load path, or measurement distance.
Technical evaluators can ask for a tolerance chain: the set of component dimensions and adjustments that collectively determine the final test position or applied condition. This approach is more informative than reviewing isolated machining drawings. A station may use accurately manufactured parts yet still have poor system-level repeatability if adjustments are not referenced, assemblies accumulate clearance, or replacement parts cannot be installed in the same position.
Useful evidence includes datum schemes for fixtures, flatness verification for support planes, calibration traceability for instruments, documented setup parameters, and controlled procedures for replacing wear components. None of these records guarantees a good measurement by itself. Together, they show whether the organization treats the test system as a controlled measurement environment rather than a collection of individual devices.
Separating product variation from test-system variation
The practical value of precision manufacturing becomes clearest when results are close to a specification limit or when two test stations disagree. Re-testing the module may be necessary, but repeated testing without a structured review can create more confusion. The first task is to determine whether the observed difference follows the module or follows the station.
A disciplined investigation normally starts with the least invasive checks. Confirm the module identity, configuration, stabilization condition, and test sequence. Then inspect contact points, fixture position, lead routing, support surfaces, and any recent station adjustment or maintenance activity. Changes that appear minor—a replaced contact head, a shifted stop, a different adapter, or a loosened rail—can have a larger effect than expected.
- Check repeat placement: Remove and reload the same module using the normal locating procedure. Observe whether the fixture establishes the same position without manual correction.
- Verify the contact interface: Inspect engagement, force behavior, contamination, and cable strain. Do not assume a visually connected terminal is an electrically stable one.
- Review the mechanical reference condition: Confirm that rails, pads, clamps, and support points remain at their specified settings and show no deformation or looseness.
- Compare a controlled reference artifact or stable reference module where applicable: The purpose is to identify station drift, not to force agreement by adjusting data.
- Examine environmental and instrument records: Irradiance, temperature measurement, timing, and calibration status must be reviewed alongside fixture conditions.
- Document the conclusion separately: Record whether the discrepancy is linked to module behavior, measurement setup, or an unresolved interaction between both.
This sequence avoids a common mistake: attributing every unexpected reading to module quality before confirming whether the measurement system remained mechanically repeatable. It also avoids the opposite mistake of blaming equipment whenever a module result is unfavorable. Precision-made fixtures improve the investigation because they reduce the number of uncontrolled variables and make deviations easier to detect.
Design features that support repeatable testing
Not every test station requires the same construction approach. A high-throughput production line has different needs from a laboratory performing detailed failure analysis. Still, several design choices consistently support better measurement control.
Reference datums should be explicit and accessible. Operators need a way to verify where the module sits, not merely a visual impression that it is centered. Contact assemblies should be replaceable without relying on ad hoc repositioning. Adjustment mechanisms should resist vibration and include a means to confirm their final setting. Where moving assemblies are involved, stiffness and backlash control affect more than machine appearance; they influence whether the same programmed position corresponds to the same physical position over repeated cycles.
Material selection also matters. Components exposed to repeated loading, heat, humidity, or cleaning agents can change dimensions or surface properties over time. A fixture designed only for initial accuracy may gradually lose consistency through wear, creep, corrosion, or loss of preload. Maintenance planning should therefore identify which elements are measurement-critical and establish inspection criteria before visible failure occurs.
In solar module testing, precision manufacturing is most valuable when it is connected to metrology and process discipline. Tight component tolerances without calibration records are incomplete. Sophisticated instruments mounted on unstable or poorly referenced structures are equally incomplete. Reliable results come from a chain in which module handling, fixture geometry, electrical contact, environmental control, instrumentation, and data review support one another.
When evaluating a testing capability, the most useful question is not whether the equipment looks advanced or whether a single measurement appears plausible. Ask whether the station can reproduce the same physical test condition after normal loading, adjustment, maintenance, and changeover. That is where precision-engineered hardware turns into more credible evidence for module performance, durability, and standards-based assessment.
Next:Already The FirstRecommended News
- 00
0000-00
How precision manufacturing improves accuracy in solar module testingPrecision manufacturing improves solar module testing accuracy by controlling fixtures, contacts, positioning, and load delivery for repeatable, credible results. - 00
0000-00
Do high performance spark plugs improve acceleration in daily driving?High performance spark plugs: discover when they improve daily-driving acceleration, restore smooth response, and deliver reliable ignition performance. - 00
0000-00
How Foldable screen technology limits crease growth over timeFoldable screen technology limits crease growth through advanced hinges, layered materials, strain control, and reliable durability testing. Explore what makes foldable displays last longer.
000000-00
{item.title}{item.description}Search News
Industry Portal
Hot Articles
- How precision manufacturing improves accuracy in solar module testingPrecision manufacturing improves solar module testing accuracy by controlling fixtures, contacts, positioning, and load delivery for repeatable, credible results.
- What renewable integration suppliers should prove before grid-scale projectsRenewable Integration suppliers must prove grid compliance, interoperability, safety, and lifetime support before grid-scale projects. Explore the evidence that reduces risk.
- What to verify before choosing a hydrogen storage tank supplierHydrogen storage tank supplier checklist: verify pressure ratings, certifications, traceability, safety controls, delivery capability, and lifecycle value before you buy.
Popular Tags